
IBR Steam Traps
Description
IBR Steam Trap Manufacturer in India
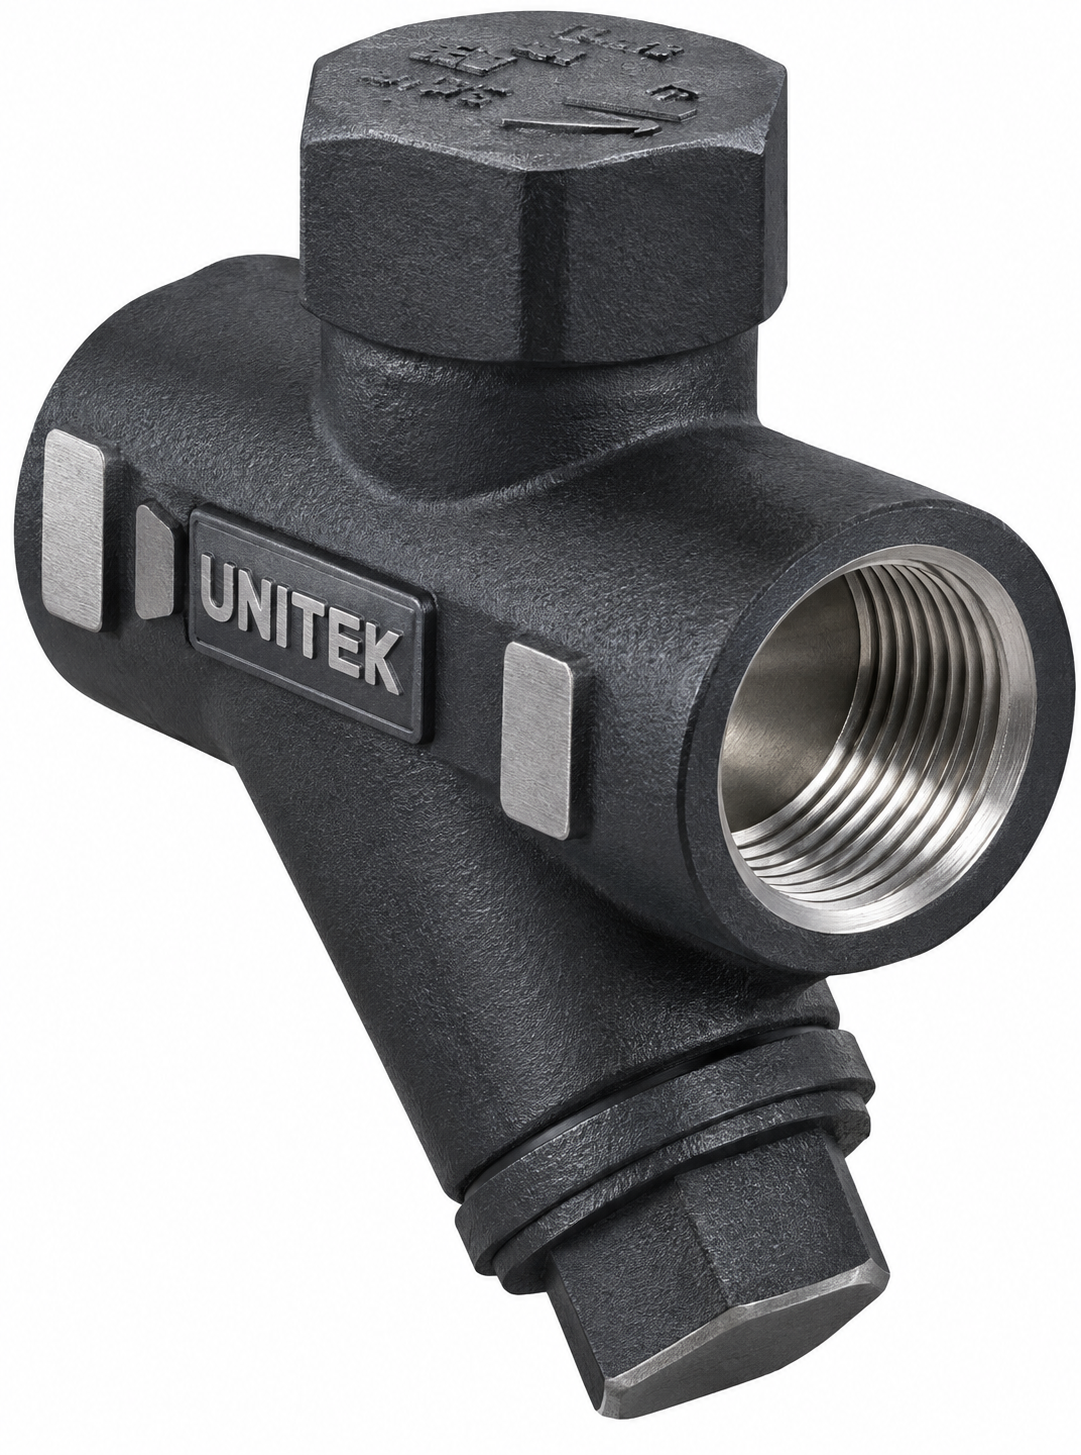
An IBR Steam Trap is an essential automatic mechanical device engineered to discharge condensate, air, and non-condensable gases from steam systems while retaining live steam as intended by the particular trap design. In industrial steam distribution networks, boiler systems, and power generation facilities, the continuous formation of condensate is an unavoidable thermodynamic reality. Efficient condensate management prevents water accumulation, protects thermal equipment, and maintains high heat transfer efficiency across process heating equipment.
Unitek Valves operates as a trusted manufacturer, supplier, and exporter of industrial valves and condensate management solutions in Mumbai, India, providing reliable steam system products for domestic industrial plants and international export markets.
What is an IBR Steam Trap?
A Steam Trap is a specialized self-contained valve that automatically differentiates between steam and condensate.
-
Condensate Discharge: Its primary purpose is to remove condensed water as soon as it forms in the piping circuit without allowing live steam to escape.
-
Gas Venting: Depending on the trap design, steam traps may also discharge non-condensable gases and air during startup and ongoing operation.
-
System Efficiency: By ensuring that heat exchangers, steam headers, and tracing lines remain free of water logging, these devices help sustain optimal thermal performance.
Note: A steam trap is an automatic drainage device; it is not an isolation valve, pressure safety valve, or pressure reducing valve.
How Does an IBR Steam Trap Work?
The general operating principle of an IBR Steam Trap relies on physical properties and thermodynamic differences between steam and liquid condensate:
-
Condensate Formation: As steam gives up its latent heat to process equipment or radiates heat through distribution piping walls, it condenses back into liquid water.
-
Trap Entry: The resulting condensate, along with any accumulated air, flows into the steam trap body under system pressure.
-
Mechanism Response: The internal operating mechanism responds to changes in temperature, density, or velocity between the steam and the condensate.
-
Discharge and Retention: The trap opens to release the accumulated liquid condensate into the return line, and then promptly closes or restricts flow to trap live steam inside the primary system.
-
Cycling: This process repeats continuously as new condensate enters the trap under changing operating conditions.
Types of Steam Traps
Steam traps are categorized into several distinct operating designs, each suited to different industrial applications:
-
1. Mechanical Steam Traps: Operate based on the difference in density between steam and condensate (such as float-and-lever or inverted bucket designs), providing continuous condensate discharge under varying loads.
-
2. Thermostatic Steam Traps: Operate based on temperature differences between steam and cooler condensate or air, utilizing thermal expansion elements to modulate discharge.
-
3. Thermodynamic Steam Traps: Operate based on the dynamic response of flash steam and condensate velocities passing through a movable disc or control chamber.
Actual trap selection depends strictly on the application, operating conditions, condensate load, and specific product design.
IBR Steam Trap for Boiler Systems
Boiler installations and associated steam generation loops generate high volumes of high-energy steam. An IBR Boiler Steam Trap is frequently installed on steam headers, drip legs, and main distribution lines to ensure dry steam delivery. Selecting a suitable trap requires careful evaluation of steam conditions, condensate load, pressure, temperature, installation location, and applicable project specifications.
IBR Steam Trap for Steam Pipelines
Steam distribution pipelines stretch across extensive industrial facilities, where heat loss through pipe walls inevitably generates condensate. Installing an IBR Steam Trap for Steam Lines at strategic points along the pipeline ensures prompt drainage of accumulated liquid. Proper condensate management along distribution headers supports reliable steam-system operation and helps protect downstream components from operational disruption.
IBR Steam Trap for Power Plants
Thermal power plants and co-generation facilities handle massive steam volumes operating at elevated pressures and temperatures. An IBR Steam Trap for Power Generation plays an important role in managing condensate across turbine steam extraction lines, auxiliary headers, and power plant utility piping, ensuring that moisture is effectively removed from high-energy steam circuits.
IBR Steam Trap for Industrial Piping & Process Steam
Industrial manufacturing relies heavily on clean, dry process steam for heating, cooking, evaporation, and drying operations. Suitable applications are found across industries such as:
-
Chemical processing
-
Petrochemical plants
-
Oil & Gas facilities
-
Power generation stations
-
Manufacturing and textile units
-
Industrial steam utilities
IBR Steam Trap Construction & Materials
A robust structural design ensures that the body shell and internal trim components withstand demanding thermal cycling, pressure forces, and corrosive condensate environments. Potentially applicable materials may include:
-
Carbon Steel: Widely specified for general steam distribution lines and industrial utility networks.
-
Cast Steel: Utilized in robust industrial applications requiring high mechanical strength.
-
Alloy Steel: Selected for high-temperature steam services requiring enhanced creep resistance.
Material selection depends strictly on steam and condensate service, operating pressure, operating temperature, corrosion conditions, specific application, and project specifications.
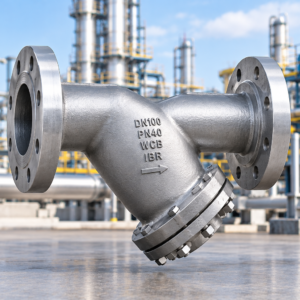
Flanged IBR Steam Trap
A Flanged IBR Steam Trap provides a secure, leak-resistant connection method for industrial piping networks. Flanged connections allow seamless alignment with standard industrial pipe flanges.
-
Piping Integration: Designed to integrate smoothly into heavy-duty industrial piping layouts.
-
Maintenance Accessibility: Flanges permit straightforward unbolting and removal when periodic inspections, cleaning, or overhauls of the drainage station are required.
-
Sealing Performance: High-performance gaskets and industrial bolting ensure reliable containment across high-pressure and high-temperature operating ranges.
Steam Trap Selection
Proper selection is vital to achieving efficient condensate removal and preventing thermal energy loss. Procurement and engineering teams should evaluate the following parameters:
-
Steam pressure and operating pressure range
-
Operating temperature limits
-
Condensate load (discharge capacity)
-
Differential pressure across the trap
-
Steam application and process requirements
-
Installation location and piping orientation
-
Drainage and return line conditions
-
Trap type classification
-
Valve body and trim material compatibility
-
End connection type and pressure rating
-
Applicable IBR regulatory standards and project specifications
IBR Steam Trap Installation & Maintenance
To ensure proper functionality, installation and maintenance practices should follow established engineering guidelines:
-
Correct Orientation: Install the trap in the correct orientation recommended by the manufacturer’s design specifications.
-
Piping Arrangement: Ensure proper sloping of upstream piping toward the trap inlet and adequate sizing of discharge lines.
-
Isolation Provisions: Provide upstream and downstream isolation valves to allow safe servicing when required.
-
Upstream Protection: Fit an appropriate strainer upstream of the trap where necessary to catch welding scale or pipe debris.
-
Accessibility: Position the trap in an accessible location for routine inspection and maintenance.
IBR Requirements, Inspection, Testing & Documentation
Compliance and documentation protocols vary based on the specific product design, service application, and contractual project specifications. Depending on order requirements, documentation scope may include:
-
Material test certificates for pressure-retaining components
-
Visual and dimensional inspection reports
-
Pressure testing and performance verification records where specified
-
Product construction and assembly documentation
-
Third-party inspection coordination, where specified by the client
-
Applicable IBR-related documentation and certification
Important: Compliance with international standards (such as ASME, API, BS, or ASTM) does not automatically confer Indian Boiler Regulations (IBR) approval. IBR applicability, approval, and documentation depend entirely on the specific equipment, application, product specification, and applicable regulatory or project requirements.
Benefits of Suitable IBR Steam Traps
-
Effective Condensate Management: Automatically drains condensed water from steam lines to maintain dry steam supply.
-
Improved Thermal Efficiency: Keeps heat transfer surfaces clear of water logging, optimizing process heating performance.
-
Equipment Protection: Safeguards downstream thermal assets and piping networks from condensate-related stress.
-
Reliable Operation: Engineered with strong body materials and proven internal mechanisms for industrial steam environments.
-
Standard Compliance: Available with required test records and regulatory documentation where specified.
IBR Steam Trap Manufacturer, Supplier & Exporter in India
UNITEK VALVES is a recognized manufacturer, supplier, and exporter of industrial valves and flow-control products based in Mumbai, India. Serving domestic processing plants and international industrial markets, the company provides dependable pipeline and condensate management solutions supported by rigorous quality control and material traceability.
The company provides dedicated support for:
-
Technical requirement review and parameter analysis
-
Product selection guidance for industrial steam and boiler applications
-
Inspection and testing coordination
-
Documentation preparation
-
Domestic supply across India and international export enquiries
How to Select the Right IBR Steam Trap
Procurement and engineering teams should evaluate system requirements systematically:
-
Identify the specific steam application (e.g., main steam line drip leg, process heat exchanger, or tracer line).
-
Determine operating pressures and maximum working temperatures.
-
Calculate or estimate the condensate load under maximum and normal operating conditions.
-
Establish the available differential pressure across the trap.
-
Select the appropriate trap operating type (mechanical, thermostatic, or thermodynamic).
-
Confirm body material, end connection ratings, and installation constraints.
-
Specify any mandatory third-party inspection or IBR documentation requirements.
Product Description
| Body : | ASTM A 351 Gr CF8 | CA15 |
| Trims : | 13 Cr | 18 Cr 8 Ni |
| Max Inlet Pressure : | 32 Kg/Cm ² AT 425 °C |
| Minimum Pressure : | 0.25 Kg/Cm ² |
| Ends : | Screwed to BSP |
| HYD Test Pressure : | 911 Psig (64 Kg/Cm ²) |
| Size Range : | 15 MM TO 25 MM |
Final Enquiry / Call to Action
Submit your technical specifications, piping datasheets, service conditions, required trap details, quantities, and applicable IBR or project requirements to UNITEK VALVES for professional engineering support and commercial quotations on IBR Steam Traps.
Only logged in customers who have purchased this product may leave a review.

Reviews
There are no reviews yet.